Once a food-factory lighting project starts, choosing the right supplier often matters more than simply comparing prices. Whether the products can withstand long-term humidity and wash-down, whether delivery stays reliable, and whether support is available when problems arise all affect normal workshop operation. After years of project support, here are practical points that help in selection.
1. Check whether the products truly match the food environment
Food plants need waterproof performance, easy cleaning and low contamination risk. The first filter is whether the fixtures offer reliable sealing and suitable materials. Suppliers that discuss only price and ignore protection and hygiene details deserve caution.
Suitable tri proof lights should be able to handle real wash-down and humid conditions.
2. Review experience with similar projects
Has the supplier completed food-processing or clean wet-area projects? Can they provide operating feedback from site? Experienced suppliers understand how ceiling height, wash-down methods and hygiene rules affect product choice, and their proposals tend to be more practical.
3. Confirm certifications, warranty and after-sales support
Are the relevant safety and protection certifications in place? Is the warranty period and coverage clearly stated? Downtime is costly in food factories, so slow after-sales response creates extra losses.
When a robust LED tri proof lamp is used in wet zones, batch consistency and uniform after-sales support become especially important.
4. Evaluate delivery capability and communication
Can lead times be committed to? Do they respond promptly to order changes? Is communication smooth? Sites usually work to fixed schedules, so supplier cooperation directly influences installation progress.
5. Compare total cost of ownership
Look at product price together with expected lifespan, energy use and maintenance frequency. A cheap option with a high failure rate may cost more after two or three years.
A well-protected weatherproof LED light reduces water and dust ingress while also lowering how often service is needed.
There is no single correct supplier, yet reviewing product fit, project experience, warranty support and delivery capability greatly reduces risk. Price matters, but it is not the only measure.
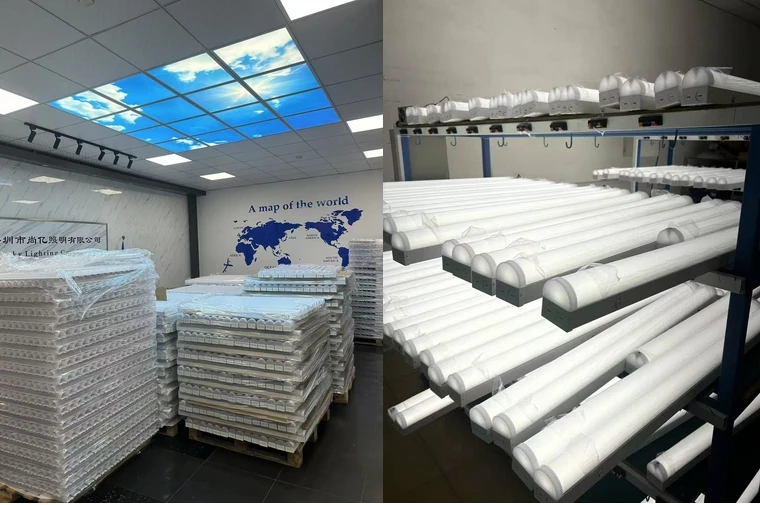
If you are selecting an LED tri-proof light supplier for a food factory or comparing several quotations, share the project scale and main environmental conditions. I can help prioritise the key points based on experience. Choosing the right partner makes the whole project more secure.